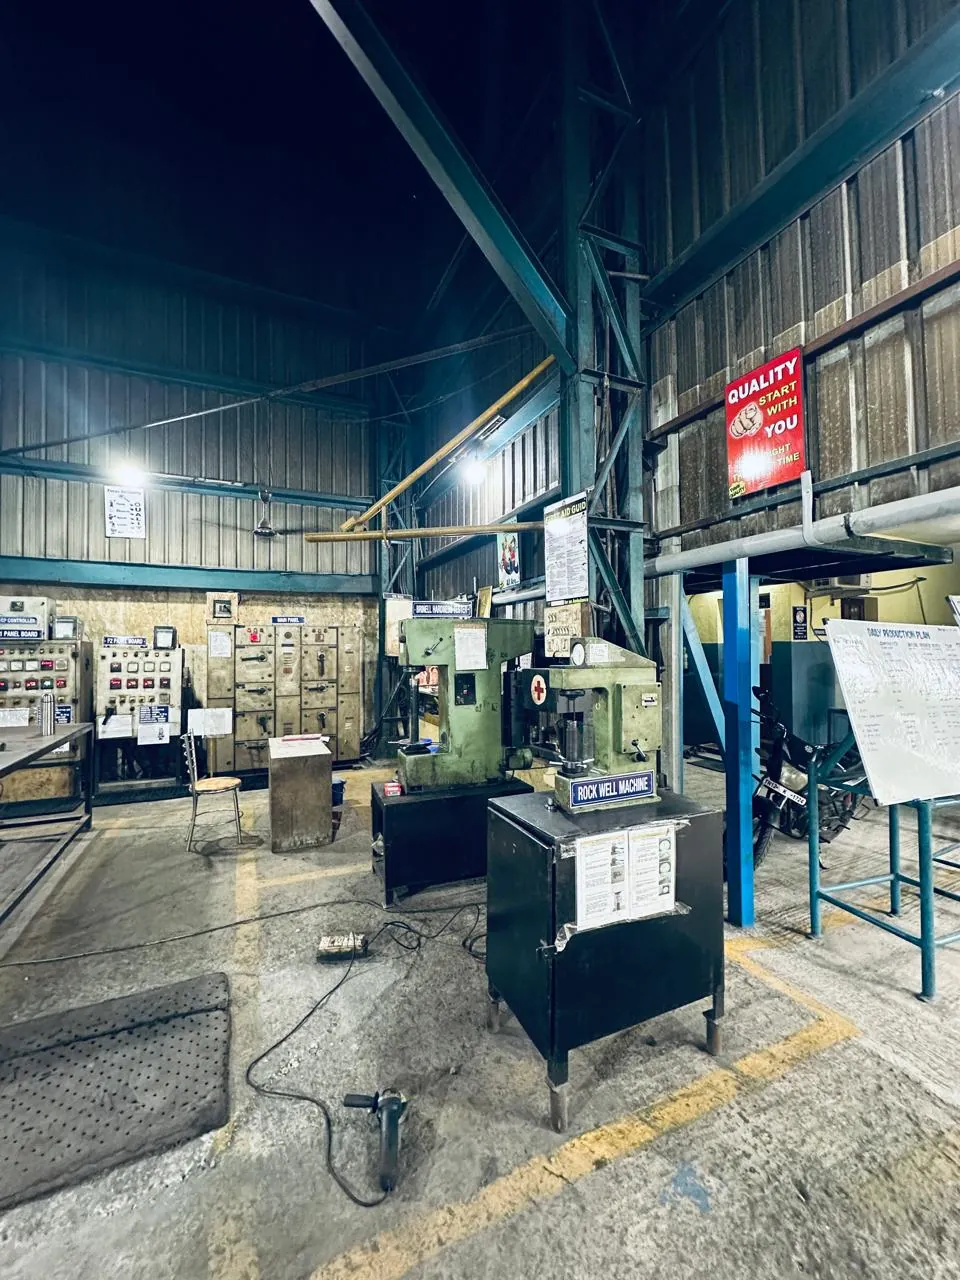
Rockwell, Brinell & optical Brinell
Rockwell, Brinell and optical Brinell-cum-Rockwell testers in house, reading at the points your drawing specifies. The number goes on the report that travels with the parts.
Quality
How we show you which one you are getting, on every batch.
Rockwell, Brinell and optical Brinell-cum-Rockwell testers in house, reading at the points your drawing specifies. The number goes on the report that travels with the parts.
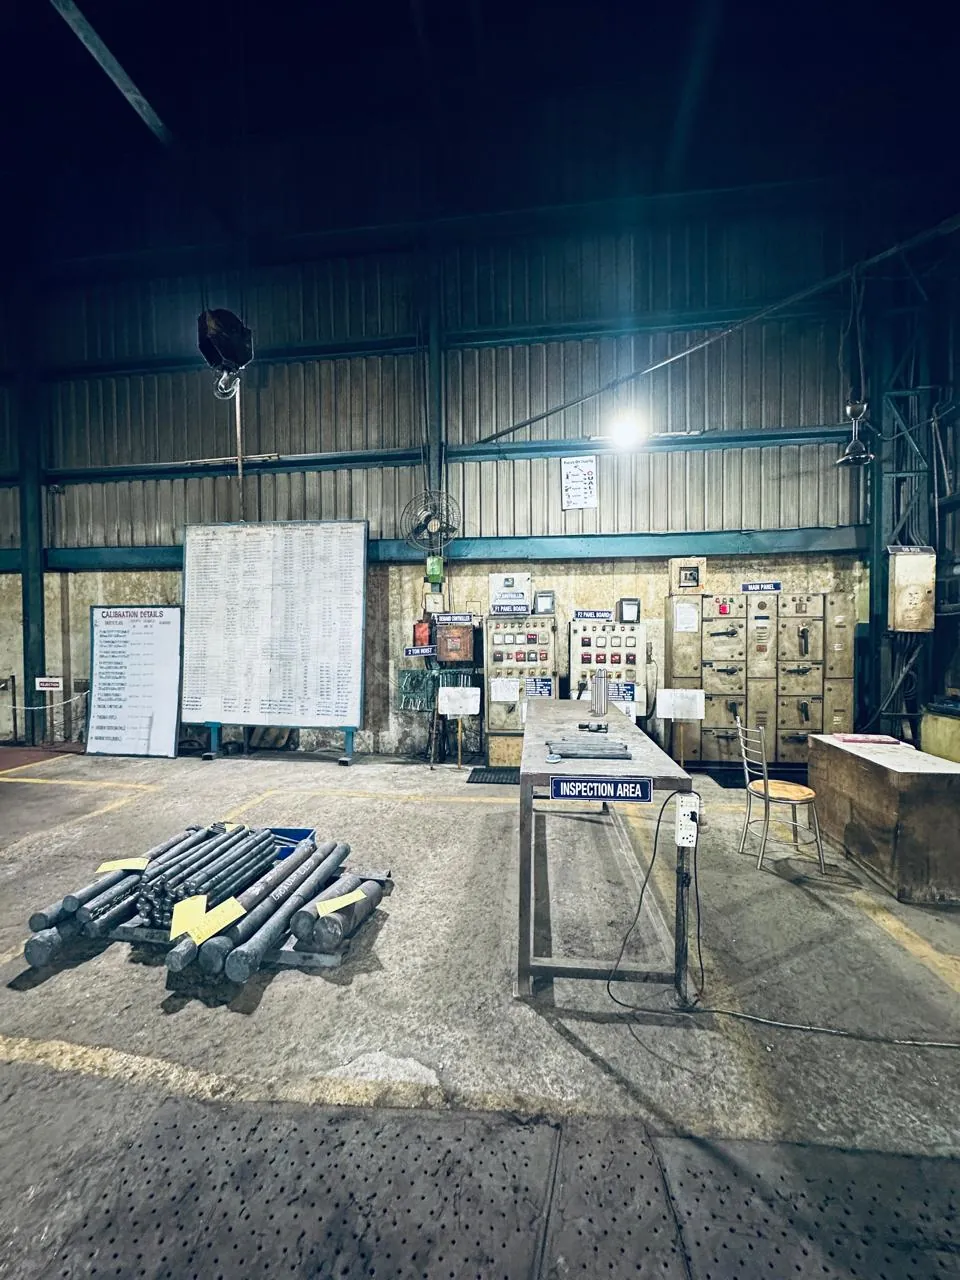
A portable tester reaches long shafts, bogie-load work and finished assemblies that will never fit under a bench machine, so big parts get the same proof as small ones.
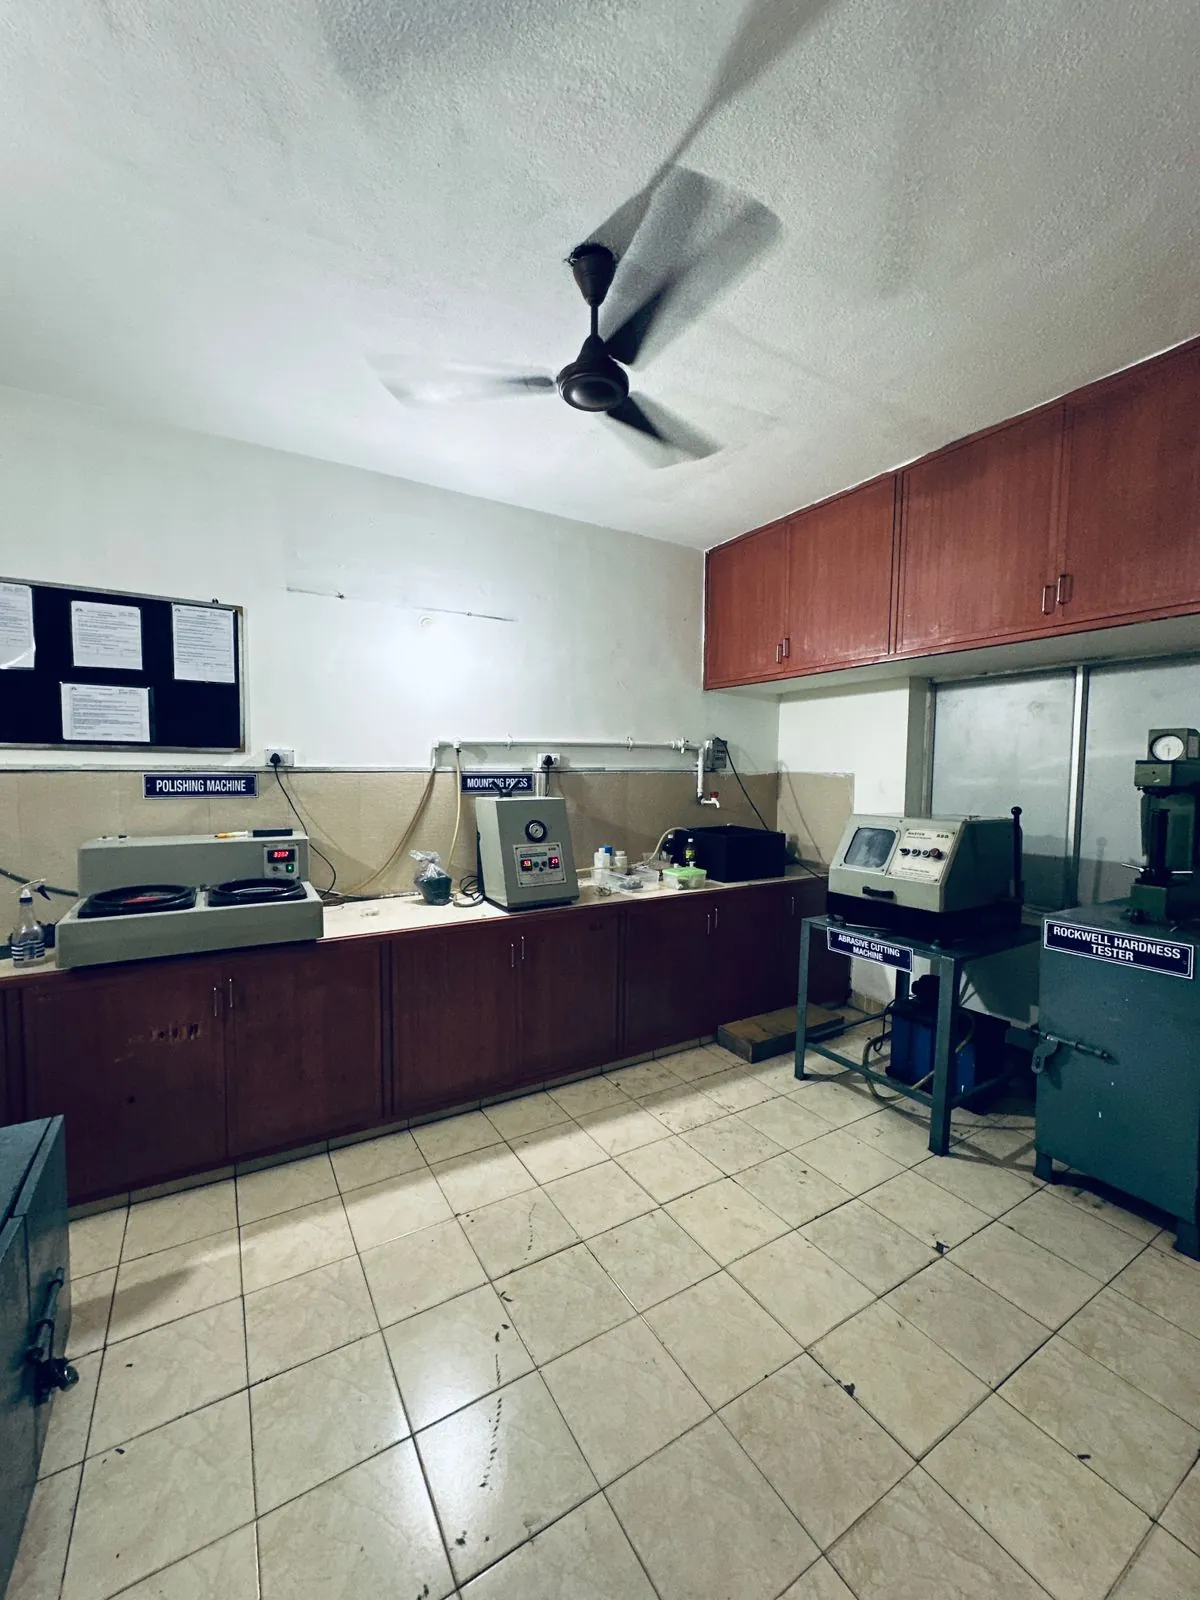
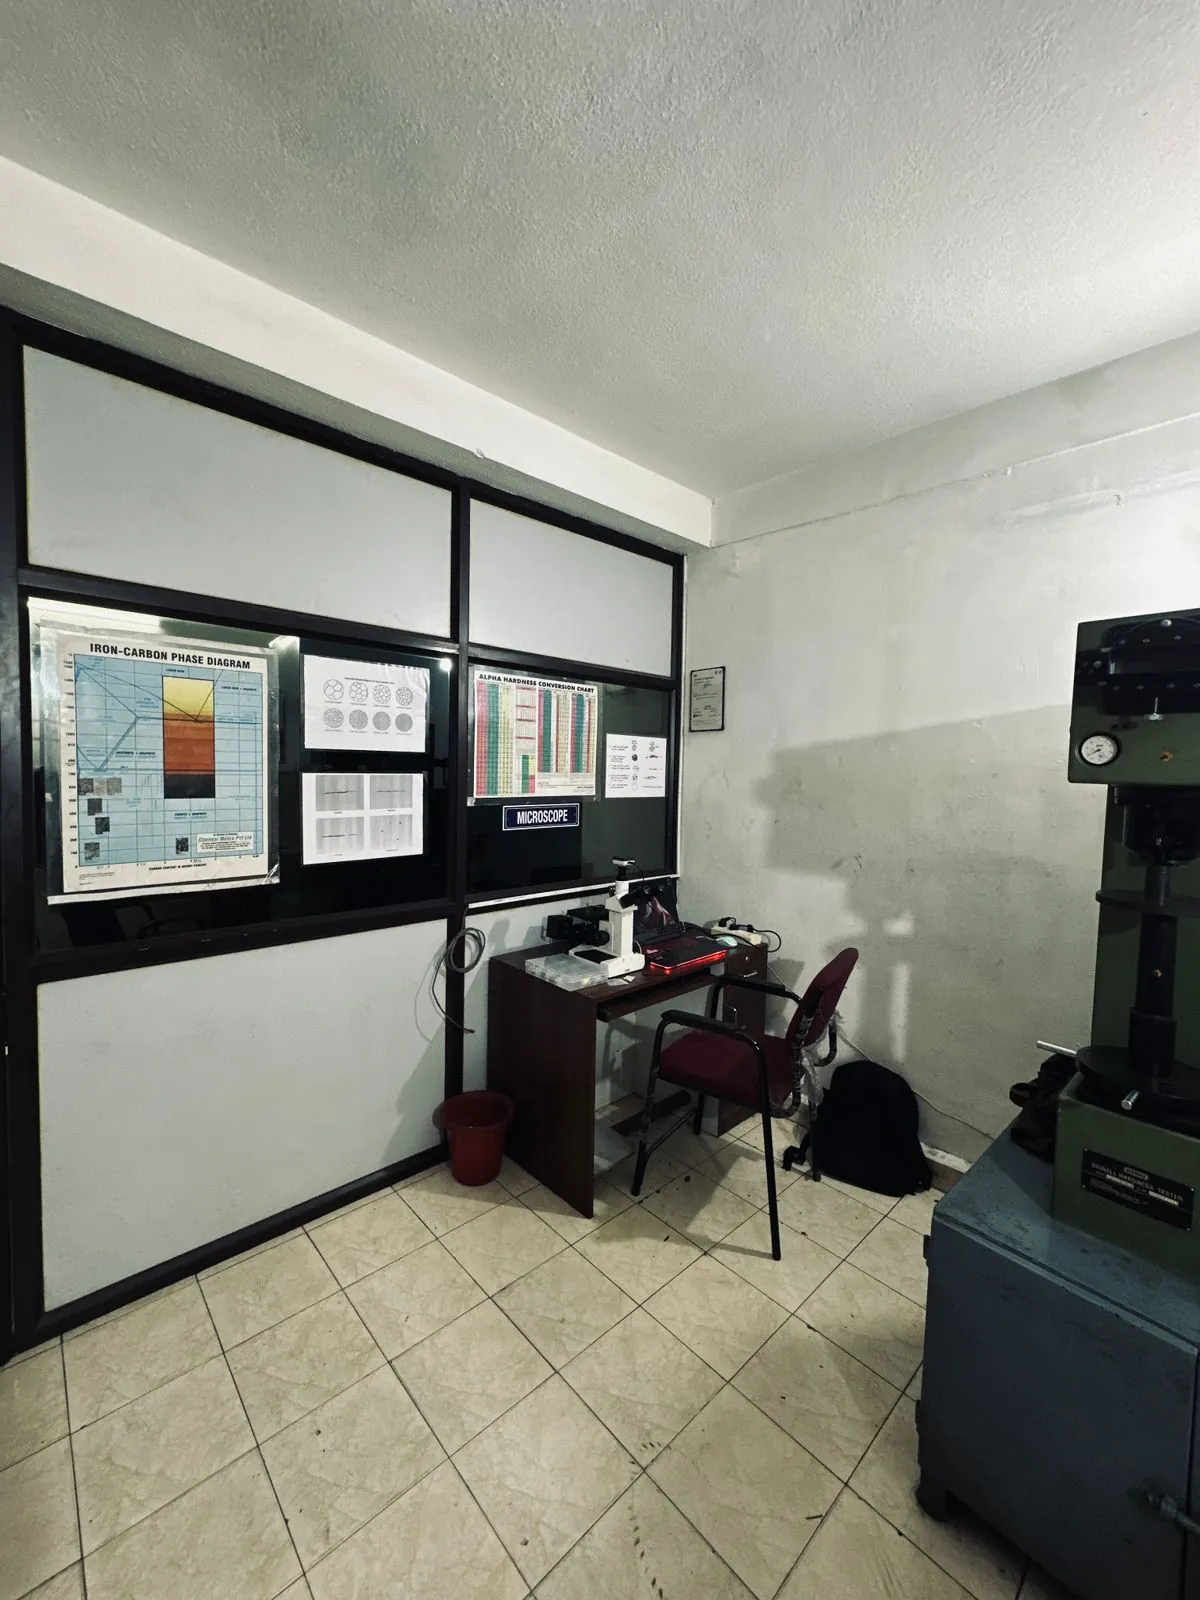
Cut on the abrasive saw, mounted, polished on the twin-disc grinder, etched and examined at up to 500×. It confirms the structure the process was meant to produce.
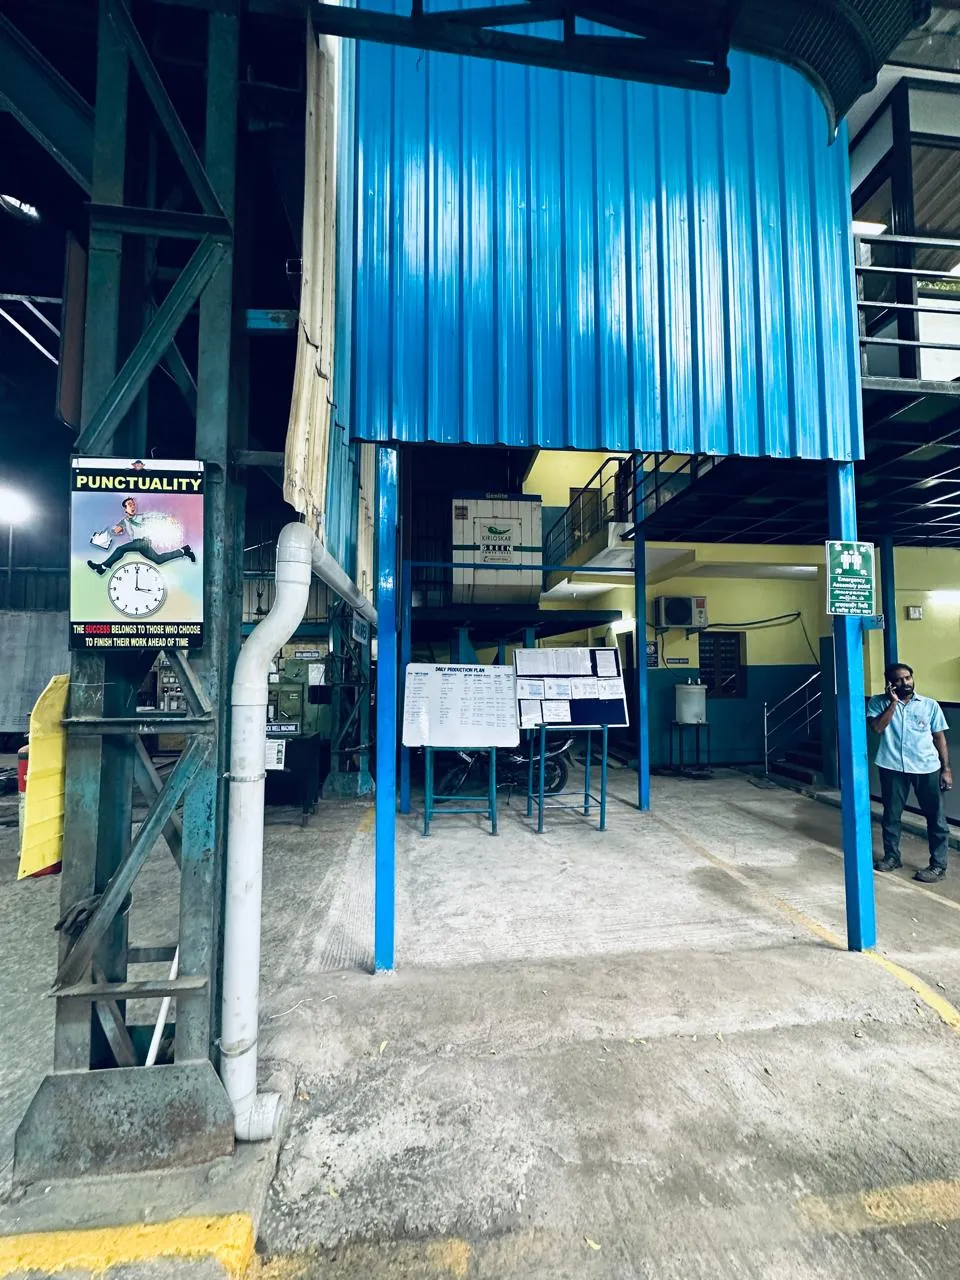
Every furnace is calibrated as per standard by an NABL-accredited lab, across 100–1050°C. Two gensets back up the power, a 125 kVA Kirloskar GenLight and a 45 kVA Powerica, so a long cycle finishes the way it started.
The system
Certified since 2006 for the heat treatment of ferrous and non-ferrous metals, and audited every year.
We work to the customer’s specification, whatever it asks for. Where there isn’t one, we follow ASTM and other general standards.
Every furnace is calibrated as per standard by an NABL-accredited lab, across its working range of 100–1050°C.
Years on the floor mean we reach the hardness you ask for, and a report travels with every batch to show it.
Policy
We commit to heat treatment that meets or exceeds what our customers expect, through standard practice and a process we keep improving.
Contact
We will get back to you soon.